Why Nozzle Size Matters
Nozzle diameter is one of the most underrated settings in FDM 3D printing. It controls the maximum layer height, the minimum feature size, the strength of vertical walls, and the total print time. A 0.2mm nozzle can resolve features a 0.8mm nozzle cannot even approach, but the same part takes 3–4 times longer to print.
Most users settle on one or two nozzle sizes and swap for specific jobs. The four sizes below — 0.2mm, 0.4mm, 0.6mm, and 0.8mm — cover every realistic use case on modern FDM printers like the Bambu Lab A1, A1 Mini, X1, P1S, P1P, H2D, H2S, and P2S.
The 0.2mm Nozzle: Ultra-Fine Detail
A 0.2mm nozzle is the detail specialist. It produces crisp text, sharp edges, and fine surface features. Miniatures, jewellery, and high-detail models benefit most. The trade-off is print time — a 0.2mm nozzle typically runs at 0.08–0.12mm layer heights, which can be 3–4 times slower than a 0.4mm nozzle at 0.2mm layer height.
0.2mm nozzles are also more sensitive to filament quality and slicer settings. Under-extrusion is more visible at this size, so well-tuned retraction and flow are essential.
- Best for miniatures, jewellery, and high-detail models.
- Layer height range: 0.08–0.12mm.
- Print time is significantly longer than 0.4mm.
- More sensitive to under-extrusion and slicer tuning.
The 0.4mm Nozzle: The Everyday Default
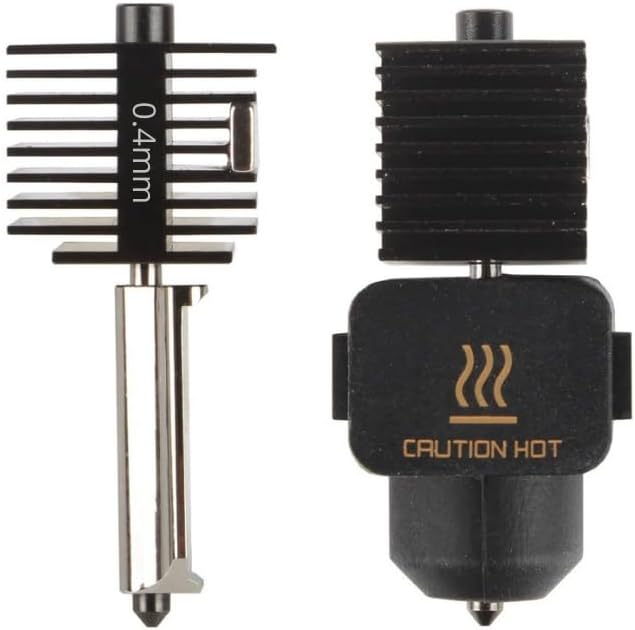
A 0.4mm nozzle is what most printers ship with, and for good reason. It strikes a balance between detail, speed, and reliability that works for the vast majority of prints. Layer height ranges from 0.12mm (high detail) to 0.28mm (draft mode) cover nearly every hobby and prototyping job.
If you only ever buy one nozzle size, 0.4mm is the safe choice. Proevove makes a hardened steel 0.4mm hotend assembly for the Bambu Lab A1, A1 Mini, H2D, H2S, and P2S that handles abrasive filaments without wearing out.
- Layer height range: 0.12mm to 0.28mm.
- Best general-purpose nozzle for most prints.
- Compatible with all standard slicer profiles.
- Hardened steel version handles abrasive filaments.
The 0.6mm Nozzle: The Speed and Strength Sweet Spot
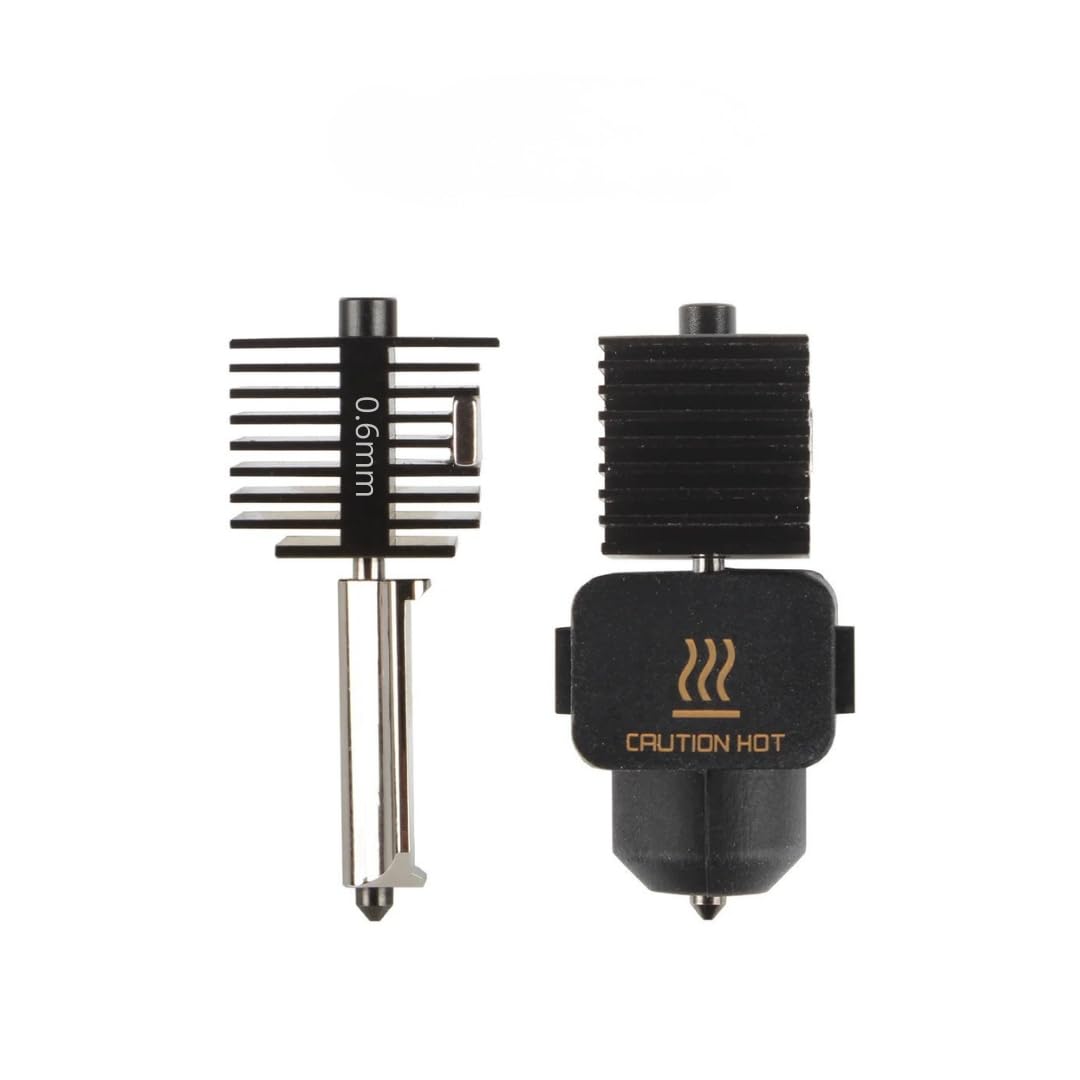
A 0.6mm nozzle extrudes more filament per pass, which means faster prints and noticeably stronger vertical walls. It is the popular sweet spot for functional parts, large prototypes, and production-style prints. Layer heights can go up to 0.32–0.36mm, cutting print time by 30–50% compared to 0.4mm at standard settings.
The trade-off is fine detail: small features, sharp text, and intricate surfaces look less crisp. For functional work, large models, and prints where strength matters more than detail, 0.6mm is hard to beat. Proevove makes hardened steel 0.6mm hotends for the A1, A1 Mini, H2D, H2S, P2S, and the X1C / P1S / P1P / X1 family.
- Layer height range: 0.16mm to 0.32mm.
- Faster prints and stronger vertical walls.
- Great for functional parts, prototypes, and large models.
- Hardened steel resists wear from abrasive filaments.
The 0.8mm Nozzle: High-Flow and Large Prints
A 0.8mm nozzle is the high-flow option. It is built for short print times on large models, thick walls, and structural parts. Layer heights of 0.4mm and beyond are realistic, and prints that would take 12+ hours at 0.4mm can finish in 4–5 hours at 0.8mm.
Detail suffers at this size — small features disappear, surface finish is rougher, and overhangs are harder to print cleanly. Reserve 0.8mm for jigs, fixtures, large prototypes, and structural parts where strength and speed matter more than finish.
- Layer height range: 0.24mm to 0.4mm+.
- Fastest prints in any given model.
- Strongest walls and thickest layers.
- Use for jigs, fixtures, large prototypes, and structural parts.
Matching Layer Height to Nozzle Size
A good rule of thumb: layer height should be 25% to 75% of nozzle diameter. For a 0.4mm nozzle that is 0.10mm to 0.30mm. For a 0.6mm nozzle that is 0.15mm to 0.45mm. Going outside this range produces poor bonding or weak layers.
Most slicers offer a layer height range input that respects these limits. Set the range to match your nozzle and you will get reliable layer adhesion and good surface finish.
- Layer height = 25% to 75% of nozzle diameter.
- 0.4mm nozzle: 0.10mm to 0.30mm layer height.
- 0.6mm nozzle: 0.15mm to 0.45mm layer height.
- Use the slicer's layer height range to enforce this automatically.
Quick Reference: Which Nozzle for Which Job?
Miniatures, jewellery, fine text: 0.2mm. General prints, everyday prototypes: 0.4mm. Functional parts, large prototypes, faster prints: 0.6mm. Jigs, fixtures, large structural parts, fastest possible prints: 0.8mm.
Most printers benefit from owning at least a 0.4mm and a 0.6mm. Add a 0.2mm if you print miniatures, and a 0.8mm if you print big. Hardened steel is recommended for any nozzle that will see abrasive filaments.
Proevove Nozzle Options for Bambu Lab Printers
Proevove makes hardened steel hotend assemblies with detachable nozzles for the Bambu Lab A1, A1 Mini, H2D, H2S, P2S, and X1C / P1S / P1P / X1 family. Available in 0.2mm, 0.4mm, 0.6mm, and 0.8mm sizes, each with a finned or extruded aluminium heatsink to prevent heat creep on long prints.
Not sure which size to add to your setup? Reach out on WhatsApp or call us — we are happy to help you choose based on what you actually print.